
How to Store Basic Welding Rods to Prevent Moisture Pickup
How to Properly Store Your Basic Welding Rods to Prevent Moisture Contamination
For shop managers and welders engaged in code-sensitive fabrication, the integrity of every weld is paramount. While skill and the right equipment are crucial, the condition of your consumables plays an equally vital role. A low-hydrogen or basic welding rod, such as an E7018, is designed to produce high-quality, ductile welds with excellent mechanical properties. However, its greatest strength—the low-hydrogen coating—is also its greatest vulnerability. Improper storage can allow this coating to absorb atmospheric moisture, reintroducing hydrogen into the weld pool and creating a significant risk of hydrogen-induced cracking and porosity. This can lead to catastrophic weld failures, costly rework, and damaged reputations.
Understanding and implementing a strict moisture control protocol is not just a best practice; it's a fundamental requirement for structural steel, pressure vessel, and other critical applications. This guide provides a comprehensive overview of how to receive, store, handle, and recondition your electrodes to ensure they perform exactly as designed, every single time.
Understanding Why Moisture Is the Enemy of Low-Hydrogen Electrodes
The "low-hydrogen" designation on an electrode like an E7018 or E7016 refers to the minimal amount of hydrogen present in the flux coating. During the Shielded Metal Arc Welding (SMAW) process, the coating burns to create a shielding gas that protects the molten weld pool from atmospheric contaminants like oxygen and nitrogen. In a basic welding rod, this coating is hygroscopic, meaning it readily attracts and absorbs water (H₂O) from the air.
When a moisture-contaminated electrode is used, the intense heat of the arc breaks down the water molecules into their constituent elements: hydrogen and oxygen. The free hydrogen atoms are then easily dissolved into the molten weld metal. As the weld cools and solidifies, the solubility of hydrogen decreases rapidly, and the trapped hydrogen atoms attempt to escape. This process creates immense internal pressure within the metal's grain structure, leading to several severe defects:
- Hydrogen-Induced Cracking (HIC): Also known as delayed cracking or cold cracking, this is the most severe defect. Microscopic cracks can form hours or even days after the weld has cooled, often invisible to the naked eye but capable of compromising the joint's structural integrity.
- Porosity: As hydrogen gas tries to escape the solidifying metal, it can become trapped, forming small, rounded voids or "pinholes" within the weld bead. This reduces the cross-sectional area of the weld, weakening it significantly.
- Embrittlement: The presence of dissolved hydrogen reduces the ductility and toughness of the weld and the heat-affected zone (HAZ), making the joint more brittle and susceptible to fracture under stress.
These risks are why welding codes like AWS D1.1 (Structural Welding Code—Steel) have stringent requirements for the storage and handling of low-hydrogen consumables. Starting with a high-quality, properly manufactured electrode is the first step, but maintaining its low-hydrogen properties until the moment of use is the welder's responsibility.
Best Practices for Receiving and Storing Unopened Packages
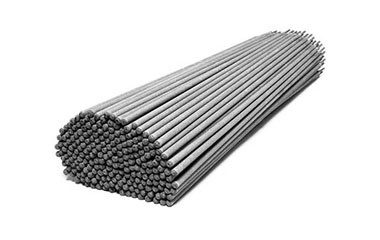
Your moisture control strategy begins the moment a shipment of electrodes arrives at your facility. Low-hydrogen electrodes are typically packaged in hermetically sealed containers—either metal cans or vacuum-sealed plastic packages—to protect them from moisture during transit and storage.
Inspection Upon Arrival
Before accepting any shipment, thoroughly inspect the packaging. Look for any signs of damage, such as dents, punctures, or broken seals. A compromised container means the electrodes inside may have already been exposed to humidity. If you find any damaged packages, quarantine them immediately and consult your supplier's guidelines. Do not introduce them into your general stock, as they will require re-baking before use.
Proper Storage Environment
Once inspected, unopened containers should be stored in a dry, controlled environment. The ideal storage area should be:
- Dry: Avoid storing electrodes in areas with high humidity, potential leaks, or on concrete floors that can transmit moisture. Store them on pallets or shelves.
- Temperature-Controlled: Keep the storage area at a stable temperature to prevent condensation.
- Organized: Implement a "First-In, First-Out" (FIFO) system to ensure older stock is used before newer stock. Clearly label shelves with the electrode type and date received.
As a global supplier serving clients in diverse climates, from the humidity of Brazil and Thailand to the varied conditions in Australia and Malaysia, we recognize the universal importance of these storage principles. A robust storage plan is the first line of defense against moisture contamination, regardless of your geographic location.
Managing Opened Packages and In-Process Electrodes
Once a hermetically sealed container is opened, the clock starts ticking. The low-hydrogen coating will immediately begin to absorb ambient moisture. This is where holding ovens become an essential piece of equipment for any professional fabrication shop.
Exposure Limits
Welding codes and manufacturer recommendations specify the maximum amount of time a basic welding rod can be exposed to the atmosphere before it must be reconditioned. While specific times vary by electrode type and ambient humidity, a common guideline from AWS D1.1 for E7018 electrodes is a maximum of four hours. For critical work, this window may be even shorter. Never leave opened packages of electrodes out overnight or over a weekend.
The Role of Holding Ovens
A holding oven is a heated container designed to keep electrodes at a temperature high enough to prevent moisture absorption but low enough to avoid damaging the coating. After an electrode package is opened, its contents should be immediately transferred to a holding oven.
- Temperature: Typical holding temperatures range from 120°C to 250°C (250°F to 480°F). Always consult the manufacturer's data sheet for the specific electrode you are using.
- Capacity: Choose an oven size appropriate for your shop's daily consumption. Overcrowding an oven can restrict airflow and lead to uneven heating.
- Portable Ovens: For field work or large fabrication yards, portable "quiver" ovens are indispensable. These smaller, mobile units allow welders to keep a limited supply of electrodes at the proper temperature directly at the point of use, minimizing atmospheric exposure.
Maintaining electrodes in a holding oven ensures they remain in a job-ready condition throughout the workday, providing welders with a consistent supply of quality consumables and preventing the defects associated with moisture.
The Re-baking Process for Compromised Electrodes
If low-hydrogen electrodes have been exposed to the atmosphere beyond the recommended time, stored in a damaged container, or otherwise compromised by moisture, they are not a lost cause. They can often be restored to their original low-hydrogen condition through a controlled heating process called re-baking or reconditioning.
When is Re-baking Necessary?
Re-baking is required when you have any reason to suspect moisture contamination. This includes:
- Electrodes from a damaged or non-hermetically sealed package.
- Electrodes left out in the open for longer than the prescribed limit.
- Electrodes that have been accidentally wetted.
- Any "mystery" rods whose storage history is unknown.
Never take a chance on questionable electrodes, especially in critical applications. The cost of re-baking is minimal compared to the cost of a failed weld.
A General Guide to Re-baking
Re-baking must be done in a dedicated rod oven with accurate temperature controls that can reach the required high temperatures. A simple holding oven is not sufficient.
Warning: The following is a general procedure. You must always follow the specific temperature and time recommendations provided by the electrode manufacturer.
- Arrange the Electrodes: Remove the electrodes from their packaging and spread them out in the oven to ensure even heat circulation. Do not re-bake electrodes directly in their cardboard boxes.
- Set the Temperature: The re-baking temperature for a typical E7018 electrode is often in the range of 370°C to 430°C (700°F to 800°F).
- Set the Time: The duration at the specified temperature is typically one to two hours. The timer starts only after the oven and its contents have reached the target temperature.
- Transfer to Holding Oven: After re-baking is complete, do not turn the oven off and let the electrodes cool inside. Immediately transfer them to a holding oven set at the appropriate holding temperature (e.g., 120°C / 250°F) to prevent them from reabsorbing moisture as they cool.
Limits on Re-baking
It's important to note that re-baking is not an infinite solution. The repeated heating and cooling cycles can eventually degrade the flux coating. Most manufacturers recommend that their electrodes be re-baked only once. Keep a log to track which batches of electrodes have been reconditioned to avoid multiple cycles.
Partner with a Supplier Committed to Quality
The foundation of a good weld is a quality consumable. Your procedures for handling and storing a basic welding rod are only effective if the product you receive is manufactured to the highest standards. At Oldwelders, we operate under a stringent ISO 9001 certified quality management system to ensure every product meets exacting specifications.
Our 1000-square-meter facility houses six modern production lines with the capacity to supply 100 tons of welding consumables per day. We start with excellent raw materials—including dolomite, bauxite, and silica—which are melted at 2000°C to create the homogenous, high-performance flux coatings our customers rely on. This large-scale, controlled production environment ensures consistency from batch to batch. With a standard lead time of approximately 30 days and a minimum order quantity of 1 ton, we are structured to be a reliable supply chain partner for industrial B2B clients.
Whether you need a versatile arc welding machine or a consistent supply of premium welding materials, our commitment to quality provides the assurance you need to tackle your most demanding projects. By combining our expertly manufactured electrodes with your own rigorous storage and handling protocols, you create an unbroken chain of quality from our factory to your finished weld.