
Wind Tower Welding: Controlling Flange Distortion
Ensuring Structural Integrity: Advanced Strategies for Wind Tower Welding and Flange Distortion Control
The construction of wind towers represents a critical pillar in the global shift towards renewable energy. These colossal structures, designed to withstand immense environmental forces over decades, rely heavily on the integrity of their welded joints. Among the most challenging aspects faced by welding engineers and tower fabricators during the process-development stage is the control of flange distortion. Flanges, serving as key connection points between tower sections, must maintain precise dimensional accuracy to ensure structural stability and ease of assembly. Unmanaged distortion can lead to significant rework, assembly delays, and ultimately compromise the operational lifespan of the wind tower.
At Oldwelders, we understand the intricate demands of high-quality fabrication. Our commitment to excellence is underscored by our ISO 9001 certification, ensuring that our welding machine, welding wire, welding rod, and welding fluxes meet stringent international standards. This article delves into comprehensive strategies for managing and mitigating flange distortion during wind tower welding, offering insights crucial for optimizing production and guaranteeing the structural integrity of these vital energy assets.
Understanding Flange Distortion in Wind Towers
Flange distortion is a complex phenomenon primarily caused by the localized heating and cooling cycles inherent in the welding process. When metal is heated, it expands; upon cooling, it contracts. If this expansion and contraction are not uniform, internal stresses develop, leading to deformation. In the context of large, thick-section components like wind tower flanges, these stresses can manifest as warping, angular distortion, or shrinkage, making it difficult to achieve the tight tolerances required for proper fit-up and secure bolting.
Causes of Distortion
- Heat Input: Excessive heat input during welding is a primary culprit. Higher temperatures and prolonged exposure can lead to greater thermal expansion and subsequent contraction.
- Material Properties: The thermal expansion coefficient and yield strength of the steel used for flanges play a significant role. Steels with higher thermal expansion or lower yield strength at elevated temperatures are more prone to distortion.
- Joint Design: Poor joint design, such as an incorrect groove angle or root gap, can necessitate more weld passes or higher heat, exacerbating distortion.
- Welding Sequence: An unoptimized welding sequence can lead to unbalanced stress distribution, causing cumulative distortion.
- Clamping and Fixturing: Inadequate clamping or fixturing allows parts to move freely during heating and cooling, leading to uncontrolled deformation.
- Base Metal Thickness: Thicker sections require more heat input and larger weld volumes, increasing the potential for distortion.
Consequences of Uncontrolled Distortion
The implications of uncontrolled flange distortion are severe and multifaceted:
- Assembly Difficulties: Misaligned flanges can make it extremely challenging, if not impossible, to bolt tower sections together, leading to significant delays and additional labor costs.
- Rework and Repair: Distorted flanges often require costly and time-consuming rework, such as grinding, straightening (mechanical or thermal), or even cutting and re-welding, which consumes valuable production time.
- Reduced Structural Integrity: Even if forced into alignment, residual stresses from distortion can weaken the joint, potentially leading to premature fatigue failure under operational loads.
- Increased Costs: Beyond direct rework, distortion increases inspection costs, prolongs project timelines, and can lead to penalties for late delivery.
Pre-Welding Strategies for Distortion Control
Effective distortion control begins long before the arc is struck. Meticulous planning and preparation are paramount to minimize the risk of flange deformation during wind tower welding.
Optimized Joint Design
Selecting the appropriate joint design can significantly reduce the amount of weld metal needed and distribute stress more effectively:
- Minimize Weld Volume: Design joints to require the minimum possible amount of weld metal. Smaller weld beads mean less heat input and less contraction. For example, using a narrow gap joint design can reduce weld volume by up to 50% compared to traditional V-grooves.
- Symmetry: Aim for symmetrical joint designs and weld placements where feasible, as this promotes balanced thermal effects.
- Double-Sided Welds: Whenever possible, use double-sided welds to balance shrinkage forces. This allows for alternating weld passes on opposite sides, counteracting distortion.
- Root Gap and Groove Angle Control: Maintain tight control over root gap and groove angle tolerances. Excessive gaps require more filler material and heat, while too narrow an angle can lead to lack of fusion.
Material Selection and Preparation
- Material Quality: Ensure the use of high-quality steel with consistent properties. Variations in material composition or internal stresses can contribute to unpredictable distortion.
- Edge Preparation: Precision in edge preparation is crucial. Using CNC plasma or laser cutting ensures accurate dimensions and consistent bevels, which are essential for proper fit-up.
- Pre-Setting and Pre-Bending: In some cases, intentionally pre-setting or pre-bending the flange in the opposite direction of anticipated distortion can help. As the weld cools and contracts, it pulls the part back into the desired shape. This requires accurate prediction of distortion magnitude.
Effective Clamping and Fixturing
Rigid fixturing is one of the most effective methods to restrain parts and prevent movement during welding. The goal is to hold the components firmly in place while allowing for some thermal expansion without buckling:
- Strongbacks and Jigs: Utilize heavy-duty strongbacks, clamps, and specialized jigs that can absorb and resist the forces of thermal contraction. These should be strategically placed to distribute pressure evenly across the flange.
- Copper Backing Bars: For specific applications, copper backing bars can be used to absorb heat, reduce penetration, and offer a consistent root pass profile, thereby minimizing distortion on the back side.
- Tack Welds: Strategic and robust tack welds are essential. They should be strong enough to hold the components in alignment but placed in locations that will be subsequently consumed by the main weld, or in non-critical areas. The size and spacing of tack welds should be carefully determined.
During Welding: Process Optimization for Distortion Control
Even with excellent pre-welding preparation, the actual welding process must be meticulously controlled to prevent distortion. This involves careful consideration of welding parameters, sequence, and techniques.
Optimized Welding Parameters
The balance of voltage, amperage, travel speed, and wire feed speed profoundly impacts heat input and, consequently, distortion:
- Minimize Heat Input: The general rule is to use the lowest practical heat input that still achieves proper fusion and penetration. This often means higher travel speeds and lower amperage, where applicable.
- Travel Speed: Faster travel speeds reduce the time the material is exposed to high temperatures, limiting the zone of thermal expansion.
- Arc Energy: Precise control over arc energy is critical. For large-scale fabrication, automated systems and advanced automatic welding machine are often employed to maintain consistent parameters.
Welding Sequence Strategies
The order in which weld passes are deposited is crucial for managing stress distribution:
- Block or Skip Welding: Instead of welding continuously along the entire length, use a block or skip welding technique. This involves welding short sections in a non-sequential pattern, allowing heat to dissipate from one area before welding an adjacent one.
- Back-Step Welding: For long joints, the back-step method involves welding in short segments in the direction opposite to the overall progression, which helps to counteract shrinkage stresses.
- Symmetrical Welding: When welding on both sides of a flange, alternate weld passes from one side to the other. This balances the thermal stresses and minimizes angular distortion.
- Multi-Pass Welding: For thick sections, multiple passes are required. The sequence of these passes (e.g., weave patterns, stringer beads) should be planned to distribute heat and stress evenly.
Pre-Heating and Interpass Temperature Control
Careful temperature management is vital:
- Pre-Heating: Pre-heating the base material reduces the temperature differential between the weld zone and the surrounding material. This slows the cooling rate, allowing for more uniform contraction and reducing the risk of cracking and distortion. Pre-heat temperatures must be carefully controlled to avoid excessive heat input.
- Interpass Temperature: Maintaining a consistent interpass temperature is equally important. Allowing the material to cool too much between passes can reintroduce thermal gradients, while overheating can lead to excessive heat buildup and increased distortion.
Advanced Welding Techniques and Materials
Leveraging advanced technology and materials can further enhance distortion control:
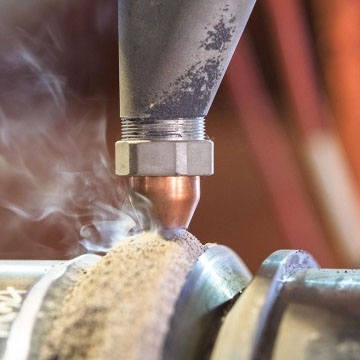
- Submerged Arc Welding (SAW): For thick flanges, SAW is often preferred due to its high deposition rates and deep penetration. Control over parameters like wire diameter and submerged arc welding flux hj431 characteristics allows for precise heat input management.
- Low-Hydrogen Consumables: Using low-hydrogen welding consumables, such as specific aws e6013 welding electrodes, can help prevent hydrogen-induced cracking, which is indirectly related to the overall integrity and stress state of the weld.
- Robotic and Automated Welding: Precision and repeatability are key. Robotic systems ensure consistent travel speed, arc length, and heat input, significantly reducing human error and variability that contribute to distortion.
Post-Welding Distortion Management and Quality Assurance
Even with the best preventive measures, some level of residual stress and minor distortion may remain. Post-welding strategies focus on rectifying these issues and ensuring the final product meets specifications.
Stress Relief and Heat Treatment
Post-weld heat treatment (PWHT) is a common method to reduce residual stresses and improve the mechanical properties of the weld and heat-affected zone:
- Full Annealing or Normalizing: For certain materials and critical applications, a full annealing or normalizing cycle can be performed to homogenize the microstructure and relieve stresses.
- Stress Relieving: This involves heating the entire structure or a localized area to a temperature below the critical transformation temperature, holding it for a specified period, and then slowly cooling it. This allows the material to yield and redistribute internal stresses.
Mechanical Straightening
For minor distortions, mechanical methods can be employed:
- Jacking and Pressing: Applying controlled mechanical force using jacks or presses can bring misaligned flanges back into tolerance. This should be done carefully to avoid inducing new stresses or cracking.
- Peening: Shot peening or hammer peening can be used on specific areas to induce compressive stresses, which can counteract tensile stresses and reduce distortion. This technique requires expertise to apply correctly.
Quality Control and Inspection
Rigorous inspection is essential at every stage, but especially post-welding:
- Dimensional Inspection: Using precision measurement tools (e.g., laser trackers, CMMs) to verify the flatness, perpendicularity, and overall dimensions of the flanges.
- Non-Destructive Testing (NDT): Techniques such as ultrasonic testing, magnetic particle inspection, and radiographic testing are used to detect internal flaws, cracks, or lack of fusion that could be exacerbated by distortion or lead to future failure.
- Fit-Up Verification: Before final assembly, ensure that mating flanges meet the specified alignment tolerances.
Oldwelders' Role in High-Quality Wind Tower Welding
At Oldwelders, we are dedicated to supporting the intricate demands of wind tower fabrication with high-performance welding solutions. Our extensive range of products, including advanced welding machine, precision welding wire, robust welding rods, and specialized welding fluxes, is engineered to meet the stringent requirements of heavy industrial applications.
We understand that the quality of materials directly impacts the success of distortion control. Our flux products, for instance, are crafted from excellent dolomite, bauxite, cryolite, silica, fluorine ore, and other high-grade ores, meticulously melted at 2000 °C to ensure superior performance and consistency. Our state-of-the-art plant, covering an area of 1000 square meters with six production lines, boasts a daily supply capacity of 100 tons, ensuring that our partners in markets like Brazil, Thailand, Australia, and Malaysia receive their essential materials reliably. We also offer a minimum order quantity (MOQ) of 1 ton, with a typical lead time of 30 days for efficient project planning.
By providing consistently high-quality welding consumables and equipment, Oldwelders empowers fabricators to achieve the precise control over heat input and weld characteristics necessary to minimize flange distortion. Our expert team is committed to partnering with welding engineers and tower fabricators, offering knowledgeable support to optimize their processes for maximum efficiency and structural integrity.
Conclusion
Controlling flange distortion in wind tower welding is a multi-faceted challenge that requires a holistic approach, integrating careful planning, precise execution, and rigorous quality assurance. By understanding the root causes of distortion and implementing proactive strategies throughout the entire fabrication process—from optimized joint design and meticulous material preparation to controlled welding parameters and post-weld treatments—fabricators can significantly reduce rework, enhance structural integrity, and ensure the long-term reliability of wind energy infrastructure.
As the demand for renewable energy continues to grow, the importance of robust and reliable wind towers will only increase. Oldwelders remains a steadfast partner in this endeavor, providing the high-quality welding solutions and expertise needed to meet the evolving demands of the industry, helping to build a sustainable future, one precisely welded flange at a time.