Electroslag Welder: Limits for Heavy Steel Welds
The Electroslag Welder: Assessing Its Limits for Heavy Steel Fabrication
For project engineers tasked with the fabrication of heavy structural sections, selecting the appropriate welding method is critical for ensuring structural integrity, efficiency, and cost-effectiveness. Among the various industrial welding processes, the Electroslag Welder stands out for its exceptional capability in joining extremely thick materials in a single pass. This method, often considered for monumental construction and heavy machinery, offers distinct advantages, but also presents specific limitations that demand careful consideration during the design and planning phases.
Oldwelders, an ISO 9001 certified manufacturer, specializes in providing robust welding machine solutions, including advanced Electroslag Welding (ESW) systems, alongside a comprehensive range of welding materials. Our commitment to quality and manufacturing excellence ensures that our clients, from target markets such as Brazil, Thailand, Australia, and Malaysia, receive equipment and consumables that meet the most demanding industrial specifications.
Understanding the Electroslag Welder Process
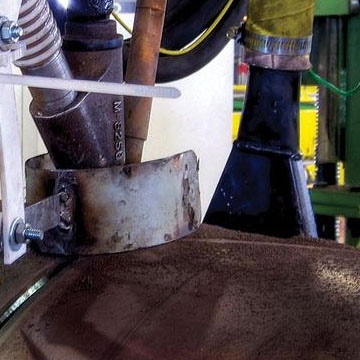
The Electroslag Welder represents a unique and highly efficient method for joining thick metal sections. Unlike conventional arc welding processes, ESW utilizes the electrical resistance heating of a molten slag bath to melt the electrode and the edges of the base metal. The process initiates with an arc between the electrode and the base metal, forming a molten pool. Flux is added, which then melts to form a conductive slag bath. Once the slag bath is established and molten, the arc extinguishes, and the current passes through the resistive slag, generating the heat required for continuous melting and deposition.
This process is typically performed in a vertical or near-vertical position, with water-cooled copper shoes or dams used to contain the molten slag and weld metal. As the weld metal solidifies from the bottom upwards, it forms a continuous, sound joint. The Electroslag Welder excels at achieving very high deposition rates and deep penetration, making it ideal for sections ranging from 25 mm to over 300 mm in thickness. The molten slag bath also serves to protect the weld pool from atmospheric contamination, contributing to the metallurgical cleanliness of the weld.
Key Advantages of Electroslag Welding for Thick Sections
The application of an Electroslag Welder brings several significant benefits, particularly when dealing with heavy steel plates and components where other welding methods might prove impractical or prohibitively expensive:
- High Deposition Rates: ESW offers exceptionally high metal deposition rates, far exceeding those of conventional arc welding processes. This translates into significantly reduced welding time for thick sections.
- Single-Pass Welding: One of the most compelling advantages is the ability to weld very thick plates in a single pass. This eliminates the need for multiple passes, reducing interpass cleaning, distortion, and overall production time and costs.
- Minimal Joint Preparation: Due to its deep penetration capabilities, ESW typically requires minimal edge preparation, often just squared-off edges, further simplifying fabrication.
- Low Distortion: The continuous, uniform heating and cooling inherent in the ESW process, combined with single-pass welding, lead to less angular distortion compared to multi-pass welding, which can accumulate distortion with each weld bead.
- Excellent Mechanical Properties: Despite the large heat input, the slow cooling rate of the weld metal within the slag bath can result in a coarse grain structure, but with careful control, satisfactory mechanical properties can be achieved, particularly in terms of toughness for the intended application.
The efficiency gained from these advantages makes the Electroslag Welder particularly well-suited for joining extremely thick plates in applications such as heavy pressure vessels, large structural columns, shipbuilding, and heavy machinery components. Our manufacturing facility, spanning 1000 square meters with six production lines, is equipped to produce the high-quality welding fluxes and equipment necessary to support such demanding projects, capable of supplying up to 100 tons of product per day. The raw materials for our flux products, including excellent dolomite, bauxite, cryolite, silica, and fluorine ore, are melted at 2000 °C to ensure superior performance.
Technical Limitations and Challenges of Electroslag Welder Application
While the Electroslag Welder offers compelling advantages for heavy steel fabrication, it is not without its limitations. Project engineers must meticulously evaluate these factors to determine if ESW is the optimal choice for their specific application:
- Coarse Grain Structure: The large heat input and slow cooling rate inherent in ESW can lead to a coarse grain structure in both the weld metal and the heat-affected zone (HAZ). This can result in reduced toughness and ductility, making post-weld heat treatment (PWHT) often necessary to refine the microstructure and improve mechanical properties, especially for applications requiring high impact resistance.
- Not Suitable for Thin Materials: ESW is specifically designed for very thick sections. It is generally not practical or economical for materials thinner than 25 mm due to the difficulty in maintaining the molten slag bath and controlling the weld pool.
- Limited Positional Capability: The process is almost exclusively limited to vertical-up welding. This restriction can be a significant constraint for complex geometries or structures that cannot be positioned vertically.
- High Heat Input: The substantial heat input can lead to significant metallurgical changes and potential issues like hot cracking if not properly controlled, particularly in certain alloy steels. Careful selection of base metals and consumables is crucial.
- Consumable Selection: The choice of electrode and flux is critical. Consumables must be specifically formulated for ESW to ensure proper slag conductivity, melt rate, and desired weld metal chemistry. Incorrect selection can lead to issues with slag detachability, porosity, or poor mechanical properties.
- Setup Complexity and Cost: Setting up an Electroslag Welder system requires specialized equipment, including water-cooled copper shoes, precise guiding mechanisms, and robust power sources. The initial investment can be higher than for conventional welding equipment.
- Lack of Operator Control: Once the ESW process is initiated, there is limited real-time operator control over the weld pool compared to manual or semi-automatic arc welding methods. Process parameters must be precisely established beforehand.
These limitations underscore the importance of thorough engineering analysis and material compatibility studies before committing to ESW for a project. Understanding the metallurgical implications and practical constraints is key to successful implementation.
Selecting the Right Electroslag Welder and Consumables
When specifying an Electroslag Welder system, engineers must consider not only the practical application but also the critical selection of consumables to ensure optimal weld integrity and performance. The quality of the welding wire, welding rod, and especially the welding fluxes, directly impacts the metallurgical properties of the final weld. For example, Oldwelders offers a minimum order quantity of just 1 ton for our flux products, making it accessible for projects of varying scales to source high-quality materials.
Key considerations for selection include:
- Base Metal Compatibility: Ensure the Electroslag Welder and its consumables are compatible with the specific type of steel being welded. This includes carbon steels, low-alloy steels, and certain stainless steels, each requiring tailored approaches.
- Mechanical Property Requirements: Assess the required toughness, tensile strength, and ductility for the application. This will guide the choice of electrode composition and flux type, especially if post-weld heat treatment is planned.
- Slag System Properties: The flux must provide a stable, conductive slag bath, protect the weld pool, and allow for easy slag removal after welding. Oldwelders' submerged arc welding flux HJ431, for instance, is engineered for consistent performance.
- Equipment Reliability: The Electroslag Welder itself must be robust and reliable, capable of maintaining stable parameters over long welding durations. Oldwelders excels in providing robust Electroslag Welder solutions, backed by our ISO 9001 certification and a 30-day guarantee on our products, reflecting our confidence in their durability and performance.
To mitigate the challenges associated with the coarse grain structure and high heat input, engineers often specify specific welding procedures that include preheating, controlled welding parameters, and, most commonly, post-weld heat treatment (PWHT). PWHT can significantly refine the grain structure, reduce residual stresses, and improve the toughness of the weld and HAZ, making the Electroslag Welder a viable option for critical applications where high impact resistance is required after treatment.
Oldwelders' Commitment to Welding Excellence
At Oldwelders, we understand the complexities involved in heavy steel fabrication and the critical role that reliable equipment and high-quality consumables play. Our extensive range of products, including various automatic welding machine options and specialized Electroslag Welder systems, is designed to meet the rigorous demands of industrial welding. Our production capabilities, with a plant covering 1000 square meters and six production lines, allow us to maintain a daily supply capacity of 100 tons, ensuring timely delivery for projects globally.
We pride ourselves on the meticulous sourcing of raw materials for our welding fluxes—utilizing excellent dolomite, bauxite, cryolite, silica, and fluorine ore—which are then melted at an intense 2000 °C to achieve superior consistency and performance. This dedication to quality is a cornerstone of our operations and extends to every product, from flux-cored wire to comprehensive welding solutions.
Conclusion: Strategic Application of Electroslag Welding
The Electroslag Welder offers unparalleled advantages for joining extremely thick steel sections, delivering high deposition rates and single-pass capabilities that significantly reduce fabrication time and costs. However, its application is contingent upon a thorough understanding of its limitations, particularly concerning metallurgical changes, positional restrictions, and the necessity for controlled procedures and often post-weld heat treatment.
For heavy steel structures, the Electroslag Welder offers unparalleled deposition rates and efficiency, but its suitability is ultimately determined by the specific material, design requirements, and a careful assessment of its technical constraints. By collaborating with experienced suppliers like Oldwelders, who provide not only advanced Electroslag Welder equipment but also expert guidance and high-quality consumables, project engineers can confidently leverage this powerful welding technology to achieve robust and cost-effective solutions for their most challenging heavy fabrication projects. The strategic application of an Electroslag Welder depends on a thorough understanding of its capabilities and limitations, ensuring successful and durable outcomes.